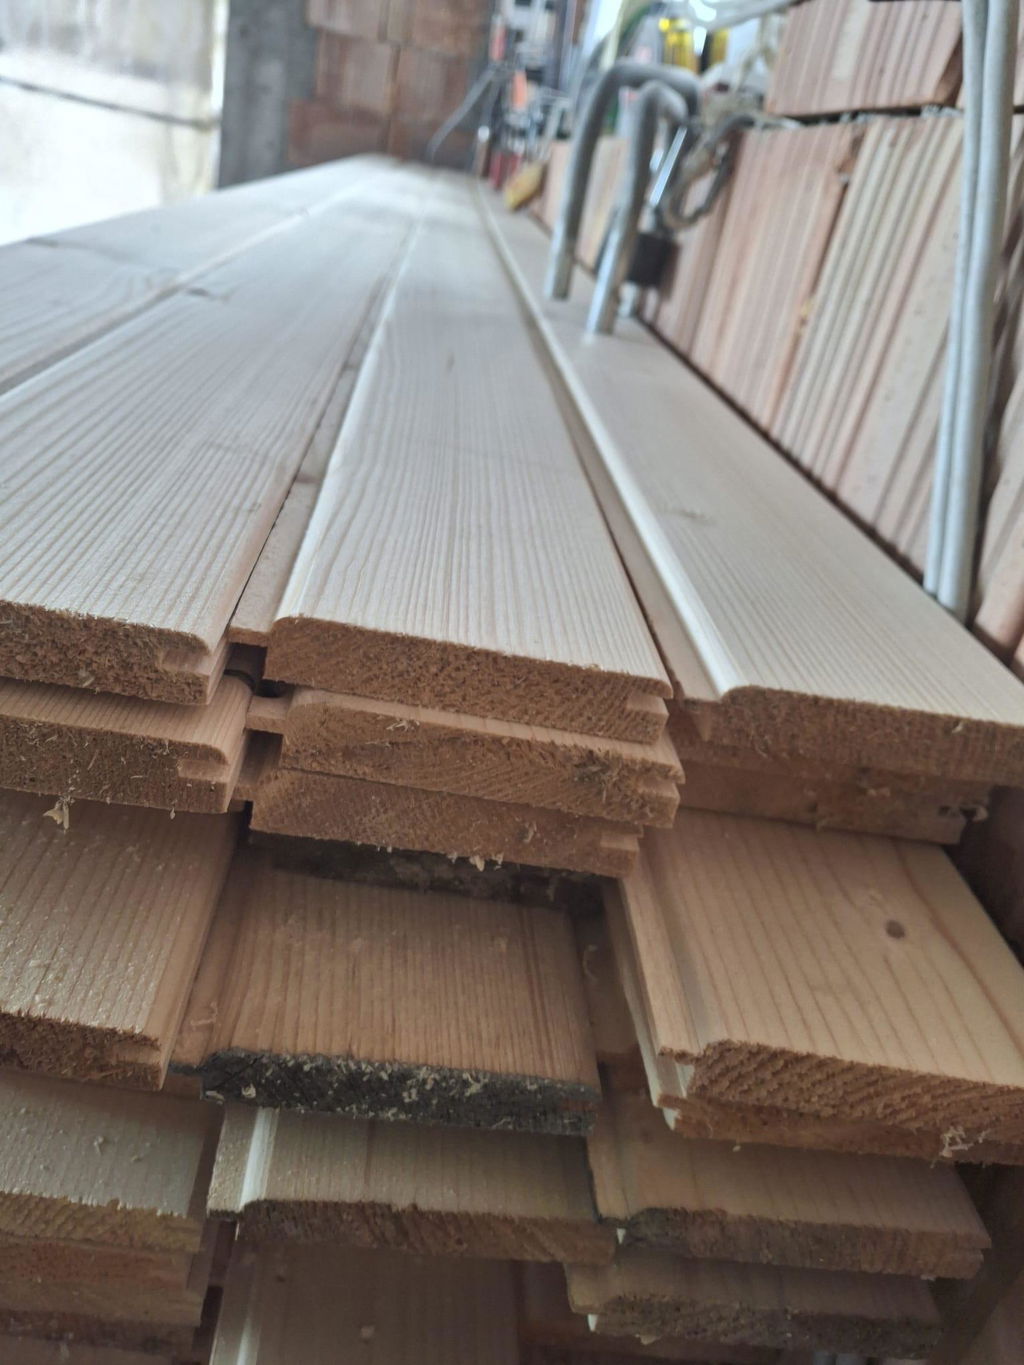
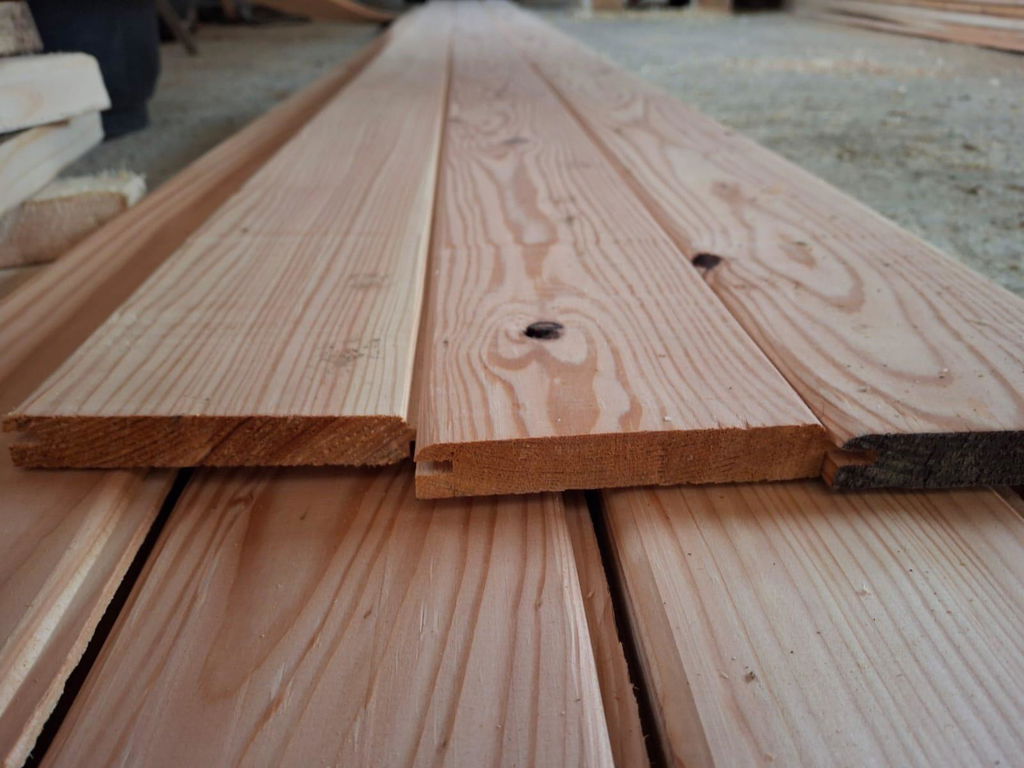
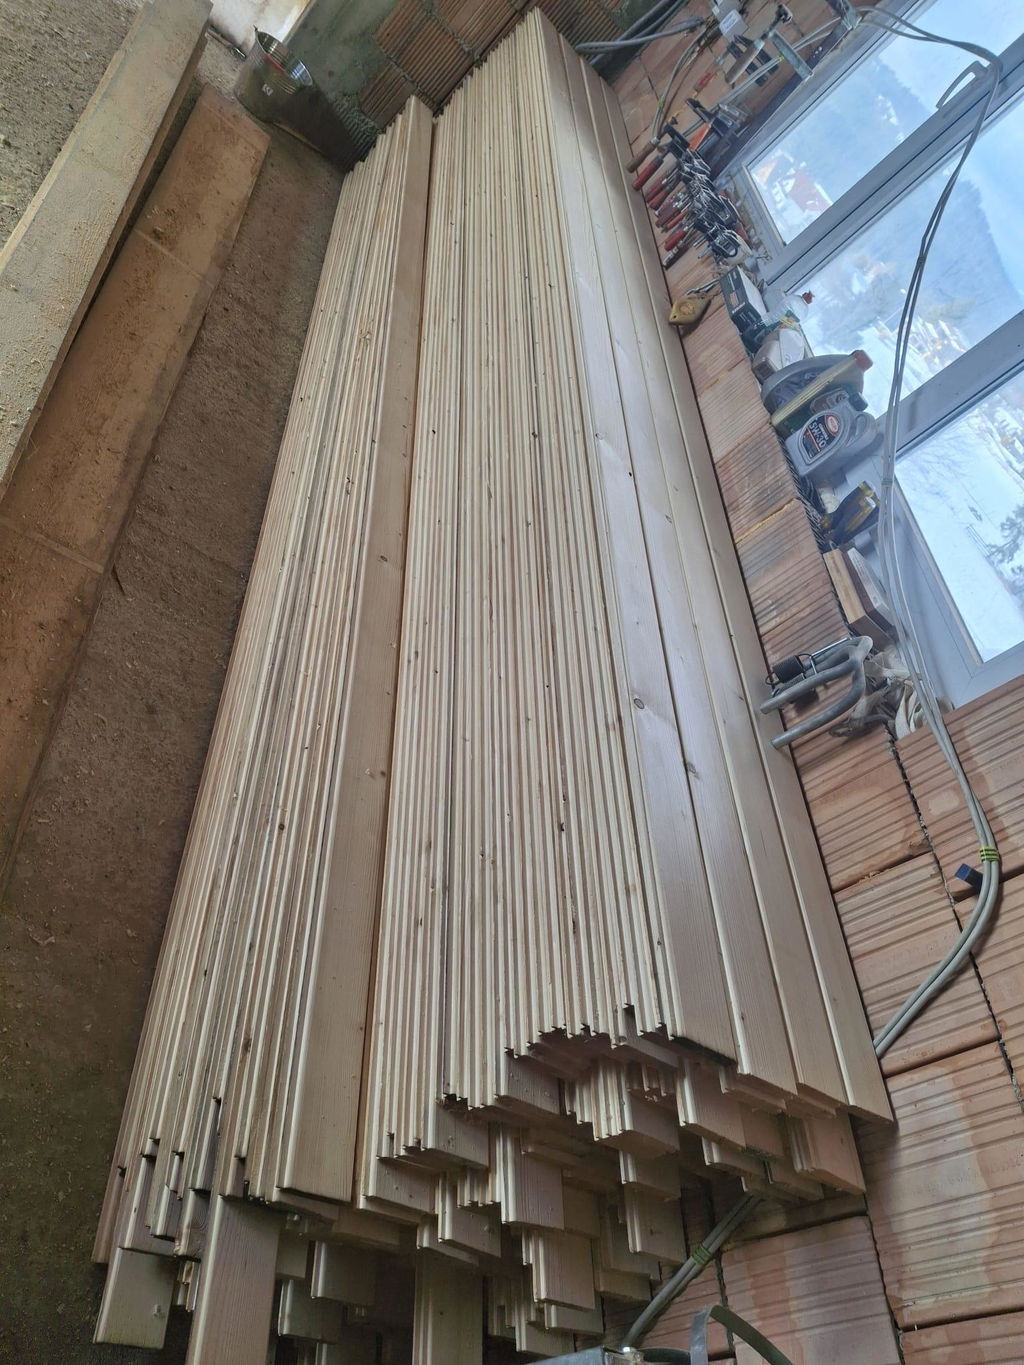
Round Profile Cladding from 16 to 26 mm – HSS M2 6.5% Tungsten
🔩 Technical Specifications:
|
Feature
|
Value
|
|
Bore (d)
|
Ø40 mm (Ø30 or Ø35 mm on request)
|
|
Outer Diameter
|
140 mm
|
|
Active Working Space
|
16 ... 26 mm
|
|
Number / Type of Teeth
|
4 pcs., brazed cutters
Inserts - HSS M2 (6.5% tungsten)
|
|
Hardness
|
63…65 HRC
|
|
Recommended RPM
|
> 9000 rpm
|
|
Wear Resistance
|
up to 3,000 linear meters in softwood
|
|
Inserts
|
Replaceable – long-term investment
|
|
Number of Cutters in Set
|
4 pcs.
|
|
Weight
|
3000g
|
🔧 Main Features:
🔹 Premium round profile cladding – allows for aesthetic and precise joints, providing an elegant and authentic wood finish.
🔹 Industrial durability – inserts made from HSS M2 (High Speed Steel), with increased wear resistance and clean cuts in any type of wood.
🔹 Workshop versatility – ideal for cladding, interior and exterior lining, decorative panels, and other solid wood carpentry projects.
🔹 Long-term investment – inserts can be resharpened or replaced, reducing costs compared to disposable cutters.
🔹 Precision for professionals and enthusiasts – designed for intensive use, but also accessible for small workshops that want quality results.
📌 With this set of HSS M2 cutters for round profile cladding, you achieve impeccable finishes and solid joints, whether you are working on a classic machine or a 4-sided moulder.
⚠️ Limitations in use:
❌ We do not recommend the HSS M2 variant for particleboard, MDF, HDF, or very hard exotic wood
❌ For composite materials or demanding applications, choose the variant with HW (K40) carbide inserts
HSS M2 COMPATIBILITY:
The cutter is mounted on most standard milling machines, being suitable for both manual work and CNC machines with moderate feed.
🛠️ Professional Selection Guide: HSS M2 vs. HW (K40)
Choosing the correct material directly influences machine performance and finish quality. Consult the technical differences below:
| Processed Material |
HSS M2 ⭐
(Choice for this set)
|
HW (K40)
(Tungsten Carbide)
|
Soft Natural Wood
(Spruce, Fir, Pine, Linden)
|
⭐ 100%
(Smooth Finish / No pulled fibers) |
80%
(Medium risk of burns at slow feed rate) |
Hard Natural Wood
(Oak, Beech, Ash, Hornbeam)
|
80%
(Clean cut / Requires more frequent sharpening) |
⭐ 100%
(Maximum wear resistance) |
Exotic / Very Hard Wood
(Mahogany, Teak, Wenge)
|
Not Recommended / Rapid wear |
⭐ 100%
(Recommended) |
| MDF / Chipboard / HDF / Agglomerates |
Forbidden / Not Recommended |
⭐ 100%
(Optimal for synthetic adhesives) |
| Cutting Edge Quality |
Maximum (Extremely fine/sharp edge) |
Standard (Chipping due to structural impact) |
| Active Layer Hardness |
63 – 65 HRC |
85 – 92 HRC |
Recommendation: For exotic or very hard woods, HW (K40) carbide cutters would be a more suitable choice.